Complex industrial installations fail most often not because of technical incompetence, but because of fragmented project delivery. When feasibility analysis sits with one consultant, design engineering with another firm, procurement with a third party, and installation with yet another contractor, the gaps between handovers become failure points. Information gets lost, accountability dissolves, and the client inherits the coordination burden.
Single-point accountability across feasibility, design, procurement, installation and commissioning keeps the same constraints in one plan. This breakdown examines how that end-to-end methodology works in practice, particularly for complex vehicle fitout projects and autonomous safety system integrations where compliance requirements are highest.
Feasibility Analysis: Establishing Project Viability
Feasibility analysis determines whether a proposed installation is technically achievable, operationally practical, and financially viable before committing resources to detailed design. For a collision avoidance system installation across a mining fleet, this phase examines vehicle compatibility, power supply adequacy, mounting locations, operator interface requirements, site communication infrastructure, and regulatory compliance pathways.
What Feasibility Analysis Actually Examines
The analysis identifies constraints early. A client may request autonomous braking integration on older haul trucks, but feasibility analysis reveals the existing hydraulic systems lack the response time for safe automation. That finding redirects the project toward collision warning rather than active intervention, preventing costly design rework later.
Risk identification forms the core of feasibility work. Site access limitations, environmental conditions, maintenance capability gaps, and supply chain vulnerabilities all surface during this phase. For remote site installations, feasibility analysis considers accommodation logistics, equipment transport constraints, and local labour availability. These operational realities shape the project scope as much as technical specifications.
Aligning on Scope Before Design Begins
Collaboration with client stakeholders during feasibility helps align success criteria. What defines project completion? Is it vehicle handover after workshop installation, or does it include operator training and several months of field support? Clarifying these boundaries prevents scope creep and establishes clear accountability.
Documentation from feasibility analysis feeds directly into design engineering. Assumptions are recorded, constraints are quantified, and preliminary resource requirements are estimated. This documentation becomes the reference point when design decisions are challenged or when project scope changes are proposed, a common occurrence on complex multi-phase programs.
Design Engineering: Translating Requirements Into Specifications
Design engineering converts feasibility findings into detailed specifications that guide procurement and installation. For a mine-spec vehicle fitout, this means electrical schematics, mounting bracket designs, wiring harness layouts, component specifications, installation sequences, and quality control checkpoints.
From Feasibility Findings to Detailed Engineering Documentation
Custom wiring harness design illustrates the level of detail required. Electrical engineering solutions sit in the same pack as the harness drawing. A standard vehicle harness cannot accommodate the additional lighting circuits, camera systems, communication equipment, and safety interlocks that mining operations demand. Design engineering specifies wire gauge, connector types, protective sleeving, routing paths, and termination methods. Each decision affects durability, maintainability, and compliance with Australian Standards.
Finite element analysis validates structural modifications before physical installation. When mounting heavy equipment to vehicle chassis or adding rollover protection structures, FEA modelling predicts stress concentrations and fatigue life. This analysis prevents field failures and ensures modifications do not compromise vehicle structural integrity.
Managing Integration Challenges During Design
Integration challenges surface during design engineering. A collision avoidance system installation requires power supply design, mounting location selection, sensor calibration, and integration with existing vehicle systems. System design holds those interfaces in one model. Design engineering resolves conflicts between competing requirements, locating sensors for optimal field of view while protecting them from impact damage, for example, before installation begins.
Review cycles with clients occur throughout design engineering. Preliminary designs are shared, feedback is incorporated, and approval is documented before progressing to detailed specifications. An elegant engineering solution that complicates maintenance or operator workflow fails in practice, regardless of technical merit. Design documentation then becomes the contract between engineering intent and installation execution.
Procurement Coordination: Managing Supply Chain Complexity
Procurement coordination bridges design engineering and physical installation. For specialised mining equipment, this phase involves vendor qualification, component sourcing, quality verification, and delivery scheduling.
Strategic Sourcing and Quality Assurance
Quality assurance protocols are non-negotiable for safety-critical components. Collision avoidance system installation uses sensors, processors, and actuators where failure could cause injury. Procurement verification includes manufacturer certification, component testing, and traceability documentation. Mining sites require evidence that installed components meet specified standards, not just manufacturer claims.
Lead time management prevents project delays. Some specialised components carry extended delivery times. 3D services can lock the as-fitted sensor and bracket positions before the next vehicle is copied. Procurement coordination sequences orders so long-lead items are ordered early while design finalisation continues on other project elements. This parallel processing compresses overall project duration without compromising design quality.
Inventory Coordination for Multi-Vehicle Programs
Inventory coordination becomes critical for multi-vehicle programs. Installing the same system across a large fleet needs parts available when each vehicle enters the workshop. Customized kits help keep later vehicles closer to the first agreed layout. Procurement coordinates bulk ordering, staged delivery, and secure storage to support installation workflow without excess inventory carrying costs.
Documentation and traceability requirements for mining industry records extend to procurement. Engineered Installations Group keeps those records with the same design pack. Every component needs a paper trail: purchase orders, manufacturer certifications, test reports, and installation records. This documentation supports later site audits and incident reviews.
Installation Management: Workshop and Field Execution
Installation management executes the design through physical work: either workshop installation services at the Forrestdale facility or field work at remote mine sites.
Workshop-Based Installation at the Forrestdale Facility
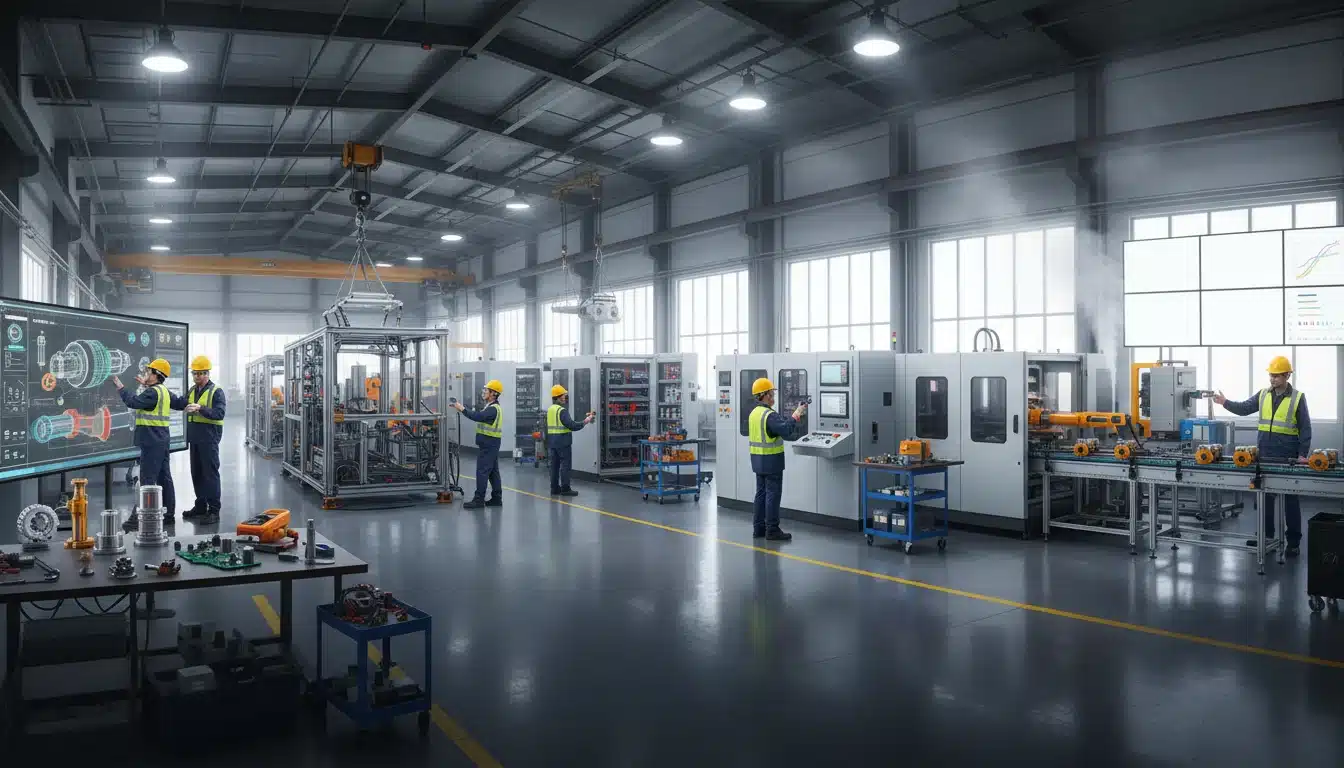
Workshop-based installations offer controlled environments, specialised tooling, and efficient workflow. A mine-spec vehicle fitout in the Forrestdale facility proceeds through defined stations: electrical system installation, equipment mounting, wiring harness integration, and pre-delivery inspection. Quality control checkpoints occur between stations, catching errors before they compound. Workshop installation services provide the physical environment and tooling precision that complex electro-mechanical fitouts require.
Real-time problem solving defines installation management. Despite thorough design engineering, physical installation reveals interferences, clearance issues, or component variations. Installation management resolves these challenges through design adaptation, alternative mounting solutions, or component substitution, always with engineering approval and documentation. This accountability loop is only practical when design and installation sit within the same organisation.
Field Installations at Remote Mine Sites
Field installations at remote mine sites introduce logistical complexity. Technician deployment requires travel coordination, site induction, accommodation booking, and tool transport. For large fleet programs, on-site installation support extends over weeks or months. Installation management coordinates these moving parts while maintaining quality standards equivalent to workshop work.
Coordination between workshop and field installations occurs frequently. Initial vehicle fitouts in the Forrestdale workshop establish a checked installation sequence, with later field work following the same method.
Commissioning and Handover: Validating System Performance
Commissioning validates that installed systems perform as specified under actual operating conditions. For a collision avoidance system installation, commissioning includes sensor calibration, detection zone verification, alarm function testing, and operator interface validation. This phase proves the system works, not just that it is installed.
On-Site Commissioning and Functional Testing
Technical site commissioning brings the checks into the operational environment. Vibration data analysis can show whether a newly mounted module is seeing more shake than the design assumed. Sensor alignment that appeared correct in the workshop may require adjustment for site-specific conditions. Communication systems tested successfully in isolation need validation within the site’s RF environment. Commissioning resolves these final integration challenges before the vehicle enters service.
Functional testing follows documented procedures derived from design engineering specifications. Each system function is tested, results are recorded, and acceptance criteria are verified. For safety-critical systems, commissioning includes failure mode testing, deliberately triggering fault conditions to confirm the system responds correctly. Technical site commissioning is not complete until every acceptance criterion is documented as met.
Operator Training and Documentation Handover
Operator training transfers system knowledge to the client’s maintenance and operations teams. Training covers normal operation, routine maintenance, troubleshooting procedures, and safety precautions. Effective training determines whether the system delivers long-term value or becomes a maintenance burden that consumes more resources than it was intended to replace.
Documentation handover provides the client with complete system information: as-built drawings, component specifications, test results, maintenance schedules, and troubleshooting guides. Final sign-off formalises project completion and transitions responsibility to the client, confirming that all contractual obligations are fulfilled, all systems perform as specified, and all documentation is delivered.
Why Single-Point Accountability Matters
The Cost of Fragmented Project Delivery
Fragmented project delivery creates accountability gaps. When feasibility analysis, design engineering, procurement, installation, and commissioning are handled by separate organisations, finger-pointing replaces problem-solving when issues arise. The client becomes the project manager by default, coordinating between contractors who prioritise protecting their scope boundaries over delivering project success.
For complex projects of this nature, fragmentation has measurable consequences. Design engineers who do not perform installations do not learn from installation feedback. Procurement teams that do not participate in design reviews do not understand which component choices affect installation time. Commissioning teams without access to design engineers cannot interpret specification intent when field conditions differ from drawings. These gaps are particularly costly on large fleet programs where vehicle availability directly affects production.
How End-to-End Engineering Lifecycle Management Narrows These Gaps
Single-point accountability through end-to-end engineering lifecycle management narrows these gaps. One organisation owns the complete process, from initial feasibility through final commissioning. Problems are solved internally rather than negotiated between contractors. Knowledge flows seamlessly between project phases because the same engineering team supports the entire lifecycle.
Risk is managed more effectively under single-point accountability. When one organisation owns the complete project, risk mitigation strategies span the entire lifecycle. Long-lead procurement items are ordered early because the project manager sees both design and installation timelines simultaneously. Installation challenges are anticipated during design engineering because installers participate in design reviews.
Quality improves when accountability is unified. Workshop installation services and field installation services follow the same quality standards, use the same documentation systems, and report to the same management structure. Cost trade-offs between design investment and installation efficiency are visible under unified project management in a way they cannot be under fragmented delivery. Spending more on robust design engineering may reduce installation time and commissioning complexity, delivering lower total project cost. These trade-offs disappear when project phases are managed across separate contractors.
The end-to-end approach keeps design, buy, install and commission under one set of records. That does not, by itself, prove schedule or budget.
For fleet fitout programs or autonomous safety systems, Contact us to check how the current installation should be staged.


Leave A Comment