A generic interval card treats two machines with the same OEM part number as if they live the same life. They do not. Payload, route, speed, terrain and time in gear change the load case on mounts, frames, wheel ends and driveline parts.
The job is to turn measured duty, a validated fatigue model and inspection findings into a reviewable schedule for one asset ID. OEM tasks and statutory inspections stay on the calendar while the overlay tracks how that asset actually works.
The engineering team brings measured duty, fatigue modelling and inspection findings together with the engineering team so the next work order belongs to that asset, not to a fleet average.
Why Generic Intervals Drift From Real Duty
OEM service books are written around design assumptions and controlled conditions. They remain the floor for warranty language, lubrication, torque checks and any inspection the manufacturer still requires. They are not a complete picture of fatigue on a machine that spends its operating hours on rough ground, variable speed or a payload near the top of the rating.
Two identical units in the same yard can still wear differently. Operator style, route assignment and shock from the ground change vibration at a given sensor point. Treating them as interchangeable on the same calendar date hides that difference until a crack, a hot bearing or a failed mount makes it obvious.
Over-servicing pulls parts with remaining life and burns crew time. Under-servicing leaves a high-duty unit on an interval that is conservative for easier work. Neither error is a reason to throw the OEM book away. It is a reason to overlay measured condition and modelled fatigue, then review the overlay when duty changes.
Statutory and site inspection controls stay in place no matter how tidy the model looks. A remaining-useful-life estimate does not replace a required crack check, a park-brake test or a scheduled OEM inspection. The written plan has to show both layers so a planner can see which task is condition-led and which task is still mandatory.
What Measured Duty Actually Records
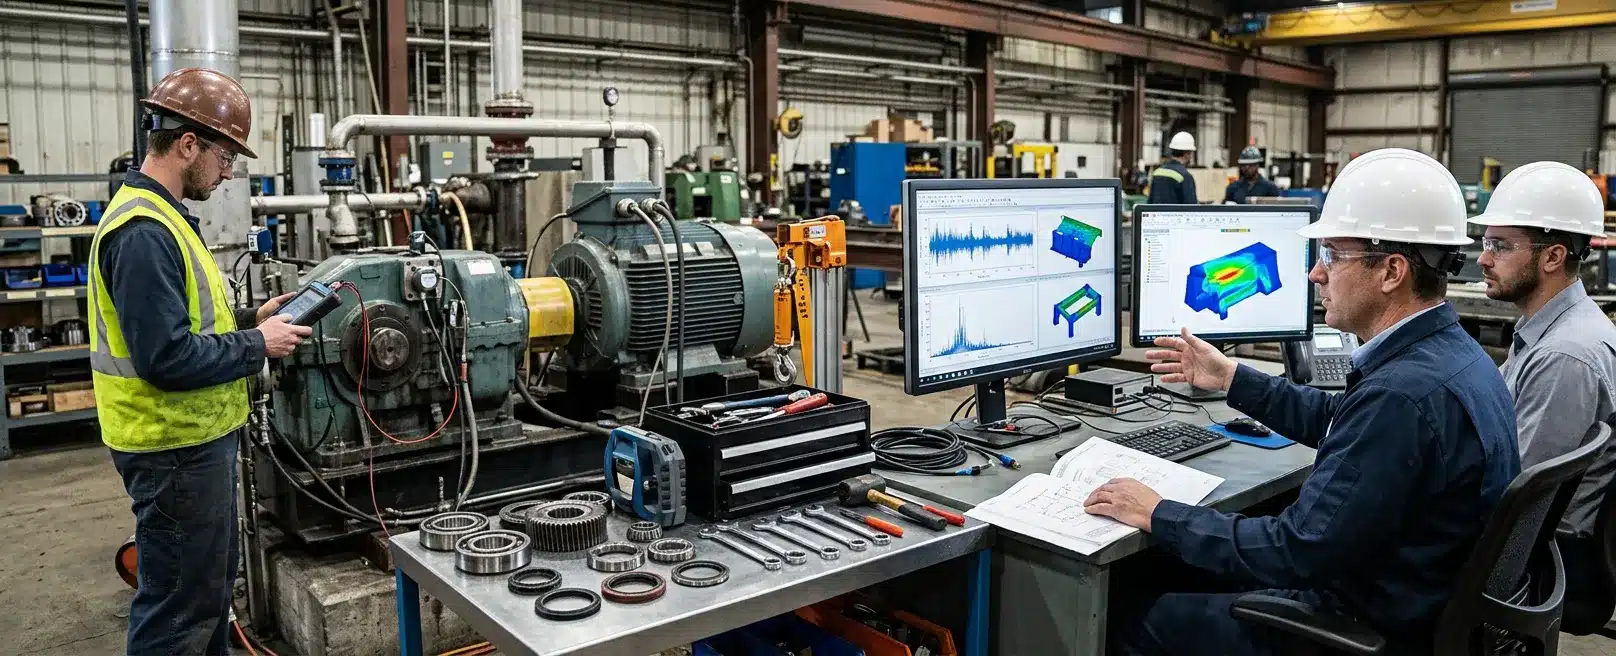
Duty is not a slogan on the asset card. It is operating hours, load, speed, terrain and how the structure and rotating parts respond. Vibration capture is how capture shows that response at chosen sensor points instead of inferring it from hours alone.
Sensor Points That Represent the Asset
Start with the failure modes that matter on this machine, not a sensor on every face. Wheel ends, final drives, gear mesh, fans, alternators, pumps and hydraulics are common mechanical sources. Structural mounts, frames and brackets matter when the question is fatigue in the metal rather than a rotating fault.
Each sensor point needs a defined location, orientation and mounting method. Poor mounting mixes noise into the signature, so check the mounting and assess which traces remain comparable. Technicians need mounting and noise-separation practice before a trace is treated as a baseline. Route-based checks and continuous logging both have a place on mobile plants that see variable speed, variable load and rough terrain.
If the machine cannot come off site, on-site installation is how the engineering team captures vibration and scan equipment in the field. If the unit can be booked into Forrestdale, workshop installation gives a controlled bay for sensor fit, post-repair acceptance checks and the first clean baseline.
Baselines, Operating Hours and Comparability
A baseline is the signature of this asset under known-good duty, tagged to operating hours and the conditions of the run. Later traces only mean something if the comparison is fair. Change the sensor point, the mounting, the sampling setup or the load case and you are no longer looking at the same series.
Not every modification invalidates history. A lighting change that does not alter mass, stiffness or the monitored path can leave the mechanical baseline intact. A new mount stiffness, a relocated sensor, a different payload band or a change to damping does need a fresh comparability check before you keep the old alarm bands.
Document payload, route, ambient conditions and who was operating when the data was taken. Without that context, a noisy shift looks like a failing bearing and a quiet idle looks like a healthy driveline. The record should let a reviewer reconstruct the duty, not only the peak number on a plot.
How Vibration Data Analysis Informs Remaining Life
The engineering team uses vibration data analysis to detect early faults in bearings, gears and driveline parts, and to manage imbalance and misalignment before they consume related components. The same traces support remaining-useful-life estimates, audit trails and CMMS integration for automated work orders and KPIs.
That is a planning function. A work order created from an alarm band tells the crew what to inspect, what parts lead time to start and when a window is justified. It does not authorise someone to stop or restart the machine. Isolation, permits and operations still own that decision.
Condition evidence also supports WHS conversations because it is objective. A rising signature at a named sensor point is easier to act on than a verbal report of a rough ride. Pre-departure checks and post-repair acceptance runs close the loop: the repair either returned the signature toward the baseline or it did not.
Start with the critical fleet, define sensor points and alarm bands, then scale. Instrumenting every asset on day one usually produces more traces than anyone reviews. A reviewed schedule on the high-duty units is more useful than an unread dashboard on the whole yard.
How Finite Element Analysis Turns Load Cases Into Fatigue Judgement
Hours and vibration describe what the asset is doing. They do not, by themselves, tell you how close a weld, bracket or frame is to a fatigue crack. That step needs finite element analysis with realistic load cases, accurate material data, sound meshing and contact, convergence checks, correlation with tests, and documented assumptions.
Raw acceleration at a sensor is not a force you can drop onto a model. Load mapping is a judgement: geometry, mass, boundary conditions and how the measured motion becomes stress in the part. Skipping that step produces a tidy plot that does not belong in a replacement interval.
Geometry, Materials and Boundary Conditions
As-built geometry matters more than a catalogue drawing when the structure has been repaired, reinforced or locally modified. 3D scanning captures the real shape of brackets, frames and mounts so the mesh is the machine in front of you, not the machine as first designed.
Material assignment has to match what is actually in service. Grade, weld procedure and whether a joint is bolted or welded change stress paths. Boundary conditions must represent the real attachment: bolt preload, weld geometry and contact, not an ideal clamp in mid-air.
Typical studies include linear and nonlinear response, modal and harmonic behaviour, transient and impact events, thermal and thermo-mechanical cases, buckling and fatigue. The analysis we run should match the question. A fatigue estimate on a cyclic mount is a different study from a one-off lifting or transport load check.
Validation Against Inspection Findings
The first fatigue model is a hypothesis. The engineering team compares predicted hot spots with cracks, wear and deformation found in the field. If the model and the inspection disagree, investigate measurement error, unmodelled duty and whether the inputs match the machine, then document the correlation and any unresolved uncertainty before you set an interval. A model that has never seen a real finding should not set a calendar date.
FEA also supports operations and retrofits: integrity of brackets, frames and mounts, and assessment of field modifications. When a new enclosure, tray or electrical cabinet is added, the question is whether the structure and the mounts still match the load case the schedule assumed.
Engineered Installations Group holds that process against the named asset.
Sensitive electrical hardware needs the mechanical answer as well as the circuit answer. Vibration findings inform mounting and damping so electrical engineering work on harnesses and schematics sits on a structure that will not shake the terminations apart. The engineering team uses system design so mechanical integration, shock, vibration, power and communication share one package, with documentation that manufacturing, installation and later maintenance can follow.
From Model and Trace to a Reviewable Schedule
The schedule is the translation layer. Measured duty says how hard the asset is working. The fatigue model says where metal is accumulating damage under those load cases. Inspection findings confirm or contradict both. The written plan then lists tasks, intervals or trigger conditions, and the evidence each line rests on.
Do not convert a fatigue plot into an automatic replacement date. Engineering judgement still sits between cumulative damage and the work order. Consequence of failure, scatter in material data, how well the model was correlated, and how much duty can change before the next review all affect how tightly you hold the interval.
Retaining OEM and Statutory Controls
Keep manufacturer inspections, lubrication, torque and replacement rules that are still in force. Keep statutory and site-required checks even when the condition data looks quiet. The overlay can add condition-based tasks, remaining-life reviews and extra crack or NDT holds. It should not silently delete a control someone else still requires.
Name the asset ID on every line. Name the sensor points and the load cases that justify a shortened or extended review. If duty is expected to change, say when the schedule itself must be reviewed, rather than waiting for a failure to force the conversation.
Tiered inspection is often more honest than a single swap date. Visual checks, then targeted crack detection, then replacement if the evidence supports it, gives the crew more than one chance to catch unexpected degradation.
Work Orders, Parts Lead Time and Crew Planning
Once alarm bands and review points exist, CMMS integration can raise a work order, help with parts lead time and give planners a KPI trail. Remaining-useful-life estimates help you order long-lead parts before the window, not after the breakdown.
Crew scheduling still needs a real outage window from operations. The analysis package should say what to inspect, what evidence would change the call, and which OEM or statutory tasks ride in the same stop. It should not pretend the model can run the shift.
After a repair, run an acceptance trace against the baseline. If the signature did not recover, the interval was not the only problem. Mounting, alignment, residual imbalance or a related part may still be in the path.
Light Ute Duty Compared With Heavy Mobile Plant
Australian light-ute fleets and heavy mobile plants should not share the same interval logic, even when they work on the same site. A ute’s GVM, braking and suspension duty is a different category from a haul unit, excavator or other heavy machine. Mixing those records contaminates both baselines.
For light utes that carry higher loads or work in harsh Australian conditions, braking and suspension upgrades change how the vehicle sits, stops and rides under load. After that work, check whether sensor points, payload band or damping have changed enough to need a new comparability run. Do not assume every upgrade changes unsprung mass or wipes the whole history. Check the configuration you actually fitted.
The heavy plant keeps its own OEM book, its own statutory inspections and its own vibration and fatigue overlay.
Named Records Before The Next Interval
The engineering team cannot write an asset-specific schedule from a part number and a rumour of rough roads. Before the engineering team models or set review points, gather the records that make the overlay reviewable.
- Asset ID and current configuration, including known modifications
- OEM and statutory task list still in force
- Operating-hours source and typical payload, route and speed band
- Existing sensor points, mounting method and any baseline traces
- Inspection history: cracks, replacements, repairs and NDT holds
- Drawings or scans of mounts, frames and any electrical cabinets on the structure
- Parts lead time for the components the model or traces are watching
- The outage window operations can actually give for capture or fit-out
If geometry is uncertain, the engineering team scans. If harness routes or control hardware sit on the structure being modelled, those drawings belong in the same pack so mounts and damping are part of one decision.
Bring those records when you discuss the project. The engineering team will use them to propose a measured-duty capture, a fatigue study that matches the real load cases, and a reviewable schedule that keeps OEM and statutory lines visible. The inspection on the day still decides what is worn. The schedule only decides when we look, what we look at, and what evidence would change the next interval.


Leave A Comment