
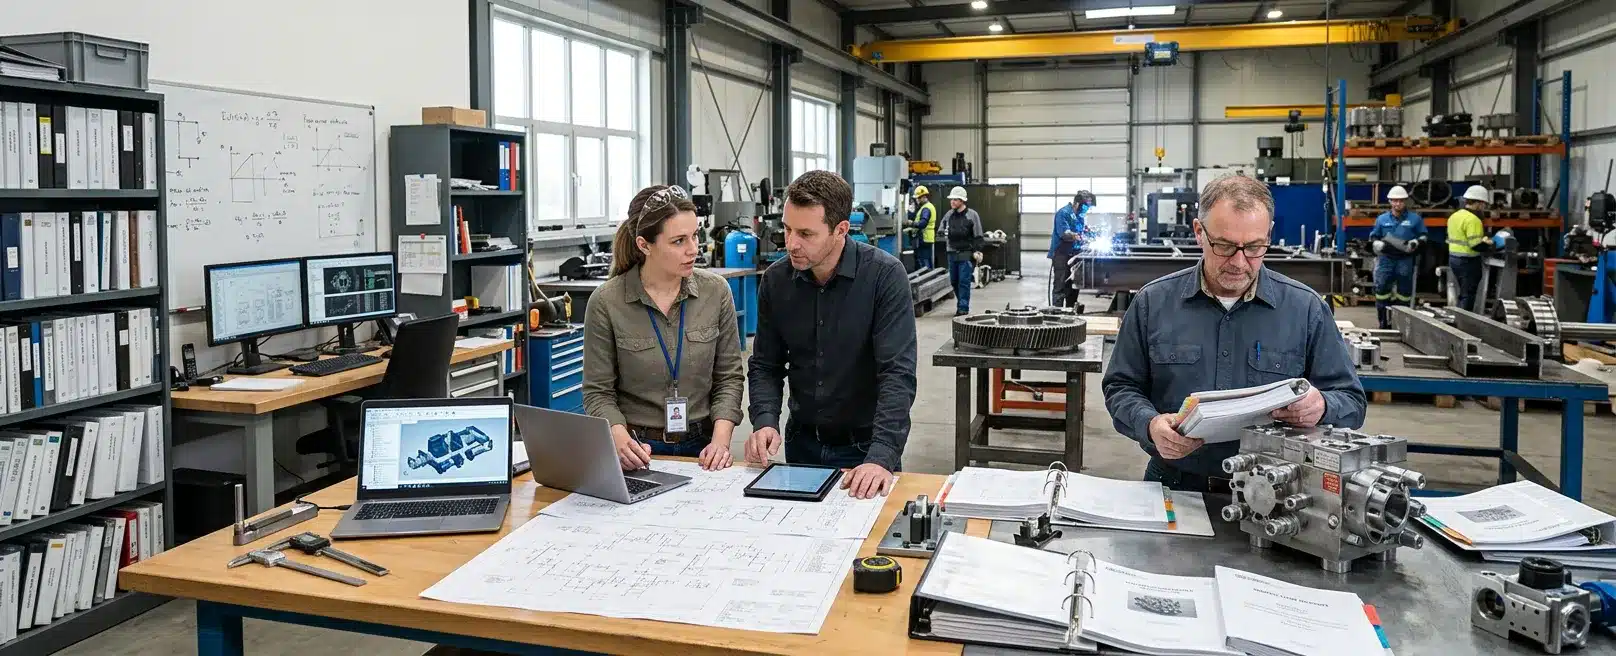
A compliance file that cannot answer a later question is not a handover. You need a record that names the requirements this asset must meet, points to the drawings that implement them, and still makes sense after someone changes a harness, a mount, or a brake kit in the field.
The engineering team brings mechanical and electrical work together with the engineering team so the record can follow one configuration, not two disconnected folders. The pack is useful when a supervisor, an OEM, or a later engineer can see what was specified, what was fitted, and what changed.
It is a chain: requirement, design evidence, installation evidence, then controlled revision. Agree that chain before fabrication starts, or you will be reconstructing it from photos and memory when the machine is already on site.
Agree Which Requirements This Deliverable Must Trace
Not every standard on a mining or transport site applies to every deliverable. A ute brake conversion and a machine emergency-stop circuit answer different questions. The first useful step is to write down which requirements this scope is meant to satisfy, and which documents will prove each one.
That list should be project-specific. Australian Design Rules are national vehicle standards for new vehicles manufactured in Australia and for imported new or second-hand vehicles being provided to the Australian market. Apply them when the vehicle and the work sit inside that market and that rule set.
Machine electrical work and safety-related controls sit under different documents. Name the duty in plain language first, then map it to a standard only where that standard actually covers the work. Holding power on a loaded ute, structural integrity of a battery enclosure, and a redundant stop circuit are three different proofs.
Mixing those proofs into one generic compliance folder hides the gap until someone asks for the wrong drawing. Keep each duty attached to the sheet, test record, and configuration identity that can actually answer it.
Separate Vehicle, Machine, And Site Duties
For Australian utes working under load, braking and suspension upgrades are a vehicle handling and stopping decision. The useful record here is the kit definition, the load and ride intent, and the installation evidence that the conversion matches that definition.
Keep that pack with the ute conversion. A roll-over protective structure test and an emergency-stop validation for plants need their own requirement maps and their own evidence.
For machinery, heavy vehicles, and mobile equipment, electrical and control work often has to show how power, communication, and safety circuits were designed to sit together. IEC 60204-1 addresses electrical equipment of machines that are not portable by hand while working, including groups of machines working together.
That document includes technical documentation among the subjects it revises. Use it where the electrical equipment of the machine is in that class. A light-ute drum-to-disc conversion follows the vehicle kit record instead.
Safety-related control design is another map. ISO 13849-1 gives a methodology for safety-related parts of control systems in high demand and continuous modes. IEC 62061 specifies requirements for the design, integration, and validation of safety-related control systems for machines. Cite the document that matches the function you are actually designing, including ISO 13850 for emergency-stop principles or ISO 14119 for interlocking devices associated with guards.
Site isolation belongs in the same handover as a work-safety record, beside the design pack rather than in place of it. Victorian plant guidance expects isolation, de-energising, lockout, and tagout before maintenance or repair, and it treats a documented isolation procedure as part of making that work safe.
The handover should show isolation points on the drawings and how those points were used during de-energised fit-out. Show the locked isolators. Keep commissioning that needs power as a separate record, taken after energy is restored under a controlled procedure. Treat emergency-stop devices as control functions on the schematic, not as the isolation method.
Write the agreed list into the job, including who owns each proof. The engineering team can prepare engineering and installation documents against that list. Keep certifier submissions, the site safety management plan, and the regulator’s approval path with the parties who own those steps.
Drawings And Analysis That Carry The Requirement
Once the requirements are named, the design pack has to carry them in a form a fitter and a later technician can use. A statement that a system is compliant is weaker than a schematic, a bill of materials, a load case, and a revision history that still match the asset.
The electrical engineering work for machinery, heavy vehicles, and mobile equipment is built around engineering-grade schematics and harness records. The schematic is the layout for the complete system and the custom wiring. Best-practice drafting reduces ambiguity during assembly and troubleshooting.
If a later change moves a termination, the revision on that sheet is what keeps the compliance story honest. Harness documentation should travel with the schematic, not live in a separate inbox.
A usable pack includes cut lists, material specifications in the bill of materials, and termination instructions. That is how you trace a failed connector back to the specified part, rather than to a substitute that never entered the record.
Integrated Functions Need One Configuration Identity
Where hydraulics, structure, power, and controls must work as one machine, system design is the place to bind those functions to a single configuration. The design process we use runs from feasibility and risk assessment, through detailed modelling, then documentation for manufacturing, installation, and certification, then support through prototyping and commissioning.
That documentation step is the hinge. Mechanical and structural integration has to show how electrical and control gear is mounted and protected against shock and vibration. Power and communication architecture has to show that added circuits do not starve the machine’s existing loads.
Safety circuits such as emergency stops and interlocks need to be drawn as the redundant functions they are, against the functional-safety documents agreed for the job. Give the configuration a revision identity early.
If the PLC map, the harness BOM, and the mechanical assembly drawing do not share that identity, later change control will argue about which file is current. Use one configuration number and one revision on every sheet that describes that build.
Geometry, Mount Loads, And Vibration Evidence
Physical integration is where compliance documentation often fails even when the circuit is correct. A battery enclosure, a camera bracket, or a control module can meet the electrical intent and still be wrong if the mount, the load path, or the vibration environment was never recorded.
Measured geometry from 3D scanning captures equipment of different sizes before you freeze routing and fastener locations. Scan data helps the as-designed mount match the real frame, tray, or enclosure.
Keep the scan identity with the CAD model and the installation drawing. A later modification can then be compared with the surface that was actually there, not with a catalogue outline.
The engineering team uses finite element analysis to quantify stress, deflection, vibration, and thermal behaviour on a proposed geometry. Typical uses include checking brackets, frames, and mounts, sizing welds and fasteners, and assessing field modifications.
For safety-critical structure, FEA can supply traceable evidence against standards such as ROPS or FOPS performance requirements, or against pressure and structural integrity cases, when those cases are in scope. That evidence is only as strong as the documented assumptions.
Record the load cases, material data, mesh and contact approach, and any test correlation. ISO 3471 specifies laboratory static-loading evaluation for metallic ROPS on listed earth-moving machine types. ISO 3449 specifies laboratory tests and performance requirements for FOPS on ride-on earth-moving machines in its scope.
File the analysis and the physical test as separate proofs in the handover. The engineering team also uses vibration data analysis when sensitive electrical hardware will live on a mobile asset. Vibration evidence informs mounting and dampening so components are not left on a resonant bracket.
Baseline signatures and an audit trail of measurement points give later maintenance a comparison. Record sensor locations, operating condition, and the alarm or acceptance band you used. A spectrum without those notes cannot defend a later change.
Environmental and network conditions may also belong on the requirement list for road and heavy-duty electrical hardware. ISO 16750-1 addresses environmental stresses and tests by mounting location for vehicle electrical and electronic systems. SAE J1455 describes environmental practices for electronic equipment on heavy-duty on and off road vehicles.
Engineered Installations Group holds that process against the named asset.
SAE J1939 is the top-level document for the heavy-duty vehicle serial control and communications network. Include these documents when the architecture actually uses those environments or that network.
Installation Evidence That Matches The Drawings
Design documents do not prove the as-fitted state. The handover needs installation evidence that a competent reader can reconcile with the current revision: what was isolated, what was torqued or terminated, what was tested, and where the work happened.
Location changes what you can verify. Controlled access during workshop installation at the Forrestdale workshop supports pre-install and post-install checks. Those checks confirm that equipment was not damaged or modified beyond the design and that the system works as drawn.
Isolation practice on that floor still matters. Technicians work to lockout, tagout, PPE, and isolation protocols so energy sources are controlled before covers come off.
The same checks look different during on-site installation because the plant around the job is often still the client’s operating asset. Field work ranges from a single-unit fit-out to a multi-site program.
The record should show how the engineering team collaborated with operations against the agreed documents, isolation, and commissioning, and which inspections were possible with the access you could give us. If a termination sits behind a guard that cannot be opened on shift, say so in the as-built notes.
Capture What Disappears After Close-Up
Some evidence only exists during the job. Fastener torque on a structural mount, crimp quality, hidden harness routing, and the isolation points used to make the work safe are difficult to reconstruct later. Photograph those steps against the drawing note they satisfy, and keep the photo identity with the revision.
Test records should name the function, the instrument or method, the result, and the configuration revision. Select tests from the functions on the agreed list. Continuity, insulation resistance, stop-circuit behaviour, communication checks, and sensor calibration prove different functions when those functions are in the job. File each result against the function it proves.
If a test could not be run because the machine could not be isolated or loaded, record the limitation. State the gap so the next engineer knows what still needs proving.
As-built drawings close the loop. Mark deviations from the issued schematic or assembly drawing, and explain why the deviation was accepted. A harness that was rerouted around a hydraulic hose is a configuration change. If it is not on the as-built, the next technician will treat the original sheet as truth and may undo a necessary clearance.
On the as-built, mark the isolation points and energy sources as they were left, including any that moved during the job. That is the picture a later isolator needs, not a reprint of the issued schematic.
NSW energy-isolation guidance treats lockout as securing an isolator in the off position, and treats tags as information rather than as the isolation device. If installers isolated the plant, the handover should list the points, the locks, and the test that confirmed zero energy before work started.
Keep The Record Alive Through Change Control
Compliance documentation fails in service when the issued pack is treated as finished the day the machine leaves. Maintenance, a component swap, or a second-system interface will create a new configuration whether you open a revision or not. Treat every later change as a controlled delta against the handover identity.
Move The Schematic And Parts List Together
Revision control should make the current sheet obvious and the superseded sheet archived and marked. Fitters should not be left with a printed harness drawing from an earlier kit. When a BOM line changes, the schematic revision, the cut list, and the as-built note should move together.
If only the purchasing file updates, the installed loom and the compliance story diverge. Maintenance traceability is the same chain used in reverse. A preventive task should point to the installation drawing and the accepted parts list so a replacement matches the specified item, or so an engineer reviews a substitute before it is fitted.
Vibration baselines and FEA load cases are part of that history when a mount or rotating assembly is disturbed. They give the conditions against which a later measurement or a later bracket design can be compared.
Agree what you need at handover, who stores the master, and how a later modification is issued back into that master. Mining sites, OEMs, and fleet workshops keep records for different reasons and for different durations. The engineering team can supply the engineering and installation files we produced for the job. Your document-control rules remain yours.
If a later change affects a safety function, reopen the requirement map, not only the parts list. An interlock, an emergency stop, or a park-brake control that is rewired for convenience is a new design question. Route it through the same schematic, analysis, and test evidence you used the first time so engineering regulatory compliance stays attached to the asset.
Specify The Handover, Then Send The Inputs That Feed It
The practical answer is a project-agreed handover record. Name the applicable requirements for this asset and this scope. Point each requirement to the drawings, BOM, analysis, and test records that implement it.
Capture installation evidence that matches the current revision, including isolation and access limits. Then keep change control on that same identity so as-built and maintenance work cannot silently replace the approved configuration.
Agree that pack in writing before manufacture or fit-out, including which proofs the engineering team will produce and which proofs remain with you or with a third party. Use that agreement for the job in front of us.
To discuss the project with enough detail to shape that record, send:
- Asset identity, duty, and where it will operate
- The requirement list you already hold, or the question you need the pack to answer
- Current schematics, BOM, and the latest revision if a system already exists
- Photographs or scan data of mount areas, isolation points, and access constraints
- Whether the fit will run in the Forrestdale workshop, on site, or both
- Known later interfaces, such as a second safety system or a planned load increase
Those inputs let us see which drawings, tests, and as-built notes the handover actually needs. The inspection and the issued revision still determine what was built.


Leave A Comment